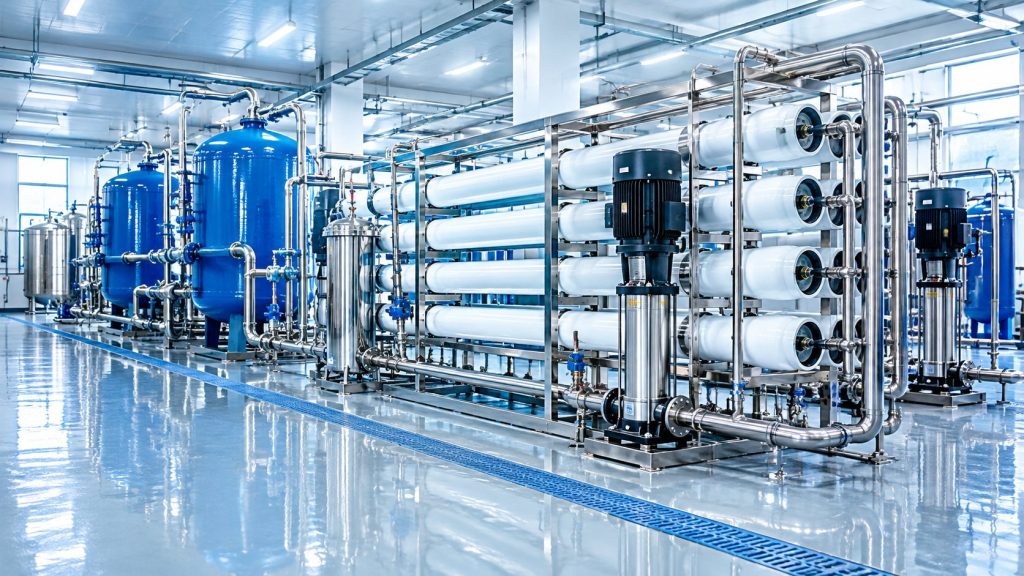
Introducing the 100T/H Reverse Osmosis System
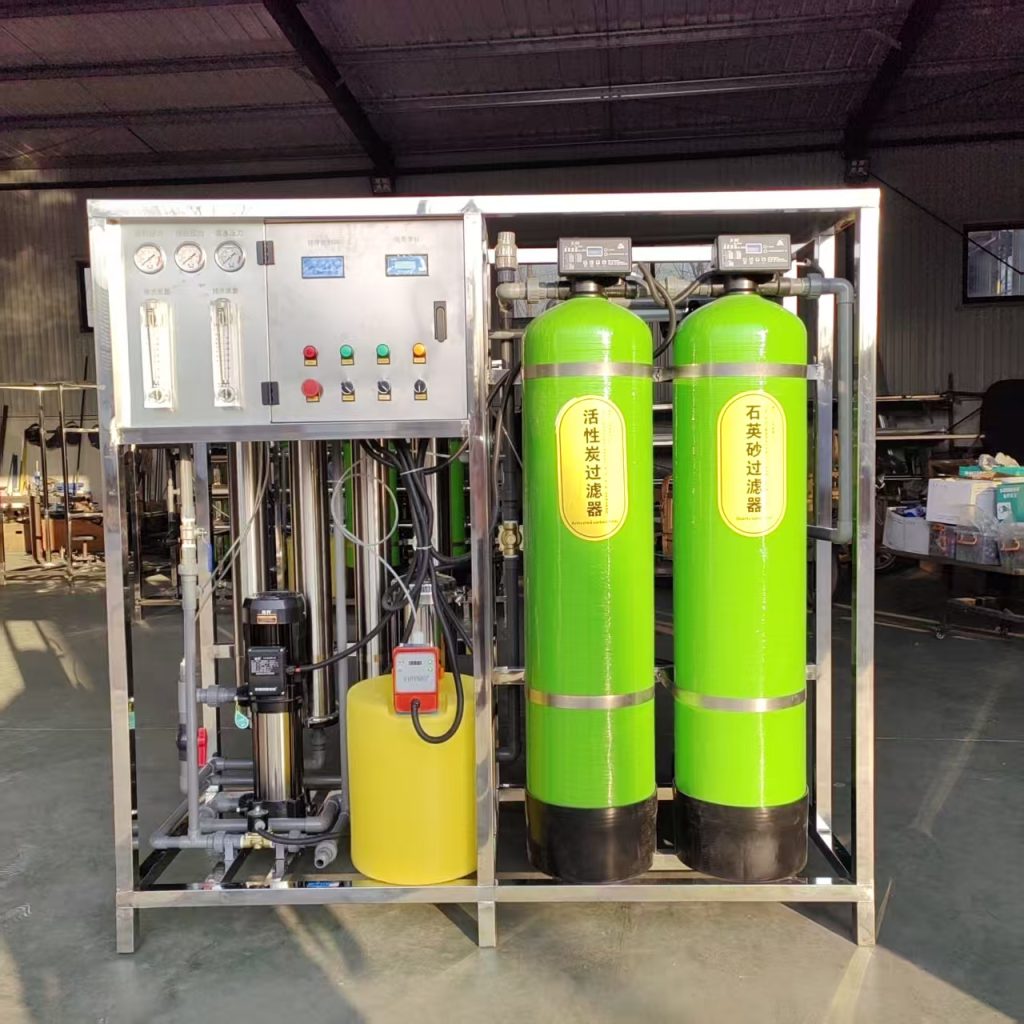
The NPW 100T/H large-scale reverse osmosis system is engineered for high-capacity industrial water purification. With a rated capacity of 100 tons per hour, this system delivers consistent, high-purity water for municipal water plants, food and beverage production, pharmaceutical manufacturing, and other demanding applications. Built with robust components and advanced RO membrane technology, it ensures reliable performance and long service life.
Key Features and Benefits
- High Flow Rate: 100T/H capacity meets the needs of large-scale operations, reducing the number of units required and saving space.
- Energy Efficiency: Equipped with high-efficiency pumps and energy-recovery devices, lowering operational costs.
- Advanced Control System: PLC-based automation with touchscreen interface for easy monitoring and adjustment.
- Durable Construction: Stainless steel housing and corrosion-resistant piping ensure longevity and hygiene.
- Comprehensive Pretreatment: Multi-media filters, activated carbon filters, and water softeners protect the RO membranes and extend their lifespan.
- Automatic Flushing: Periodic membrane flushing reduces scaling and maintains performance.
Applications
This RO system is ideal for:
- Municipal water treatment plants
- Food and beverage processing (e.g., bottled water, juice production)
- Pharmaceutical and medical water
- Industrial boiler feed water treatment
- Electronics manufacturing
Working Principle
Raw water undergoes pretreatment to remove suspended solids, chlorine, and hardness. It is then pressurized by a high-pressure pump and forced through semi-permeable RO membranes, which reject dissolved salts, bacteria, and organic matter. The permeate (purified water) is collected, while the concentrate is discharged. The system includes a CIP system (clean-in-place) for periodic membrane cleaning.
Quality Assurance and Delivery
Each NPW RO system is thoroughly tested before shipment, including performance tests and water quality analysis. The system is securely packed in export-worthy wooden cases or containers, ensuring safe delivery to any global destination. NPW provides comprehensive technical support and after-sales service to ensure seamless installation and operation.
NPW’s 100T/H RO system combines high capacity with precision engineering, offering a reliable solution for large-scale water purification needs.
For more information, visit npwequipment.com.
Solutions related to this article
 WaterWater Purification Equipment SolutionTreatment and reuse for process water, scalding tanks and plant supply.View solution →
 WastewaterWastewater Treatment Equipment SolutionScreens, flotation, clarifiers and sludge pressing for plant effluent.View solution →
 PoultryComplete Poultry Slaughter Line SolutionsHanging, scalding, plucking, evisceration and chilling on one continuous line.View solution →
Products related to this article
 WATER PURIFICATION EQUIPMENT
REVERSE OSMOSIS WATER PURIFICATION EQUIPMENT
The reverse osmosis water purification equipment adopts advanced RO reverse osmosis membrane separation technology. After the raw water is…
View product →
 WATER & ENVIRONMENTAL
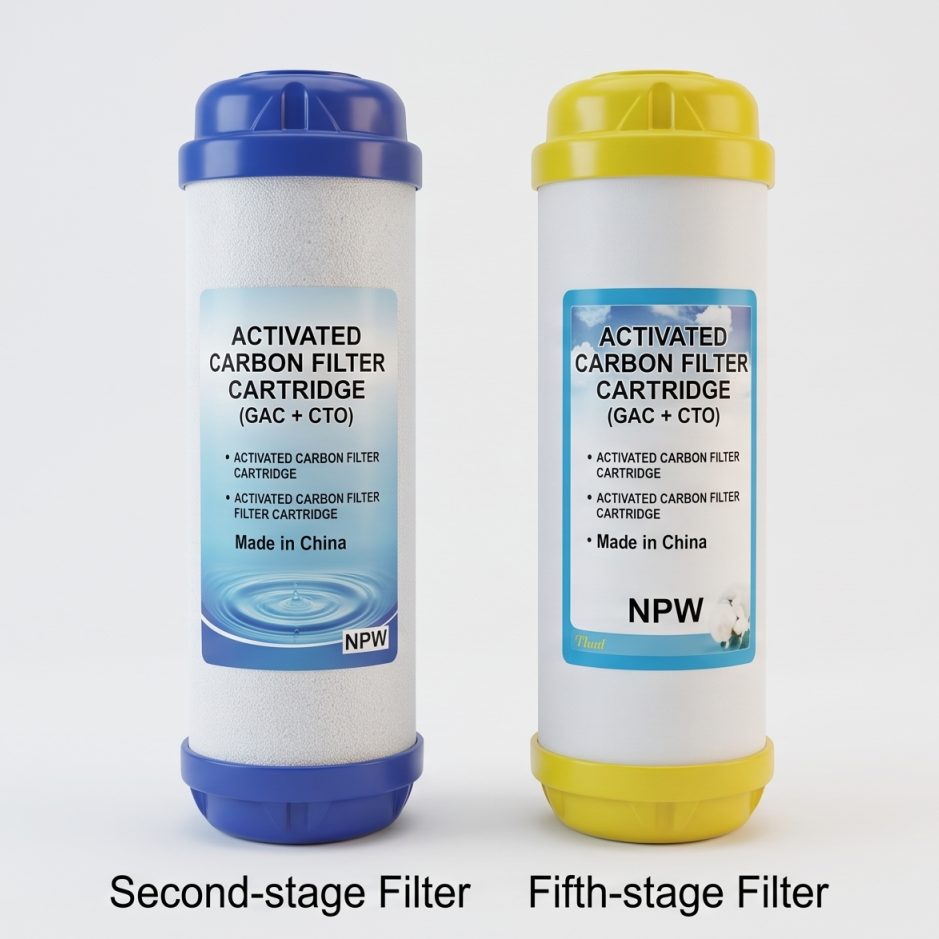
ACTIVATED CARBON FILTER CARTRIDGE (GAC + CTO)
Activated carbon filter cartridge made of imported coconut shell carbon, effectively adsorbing odor, chlorine and improving taste.
View product →
 WASTEWATER TREATMENT EQUIPMENT
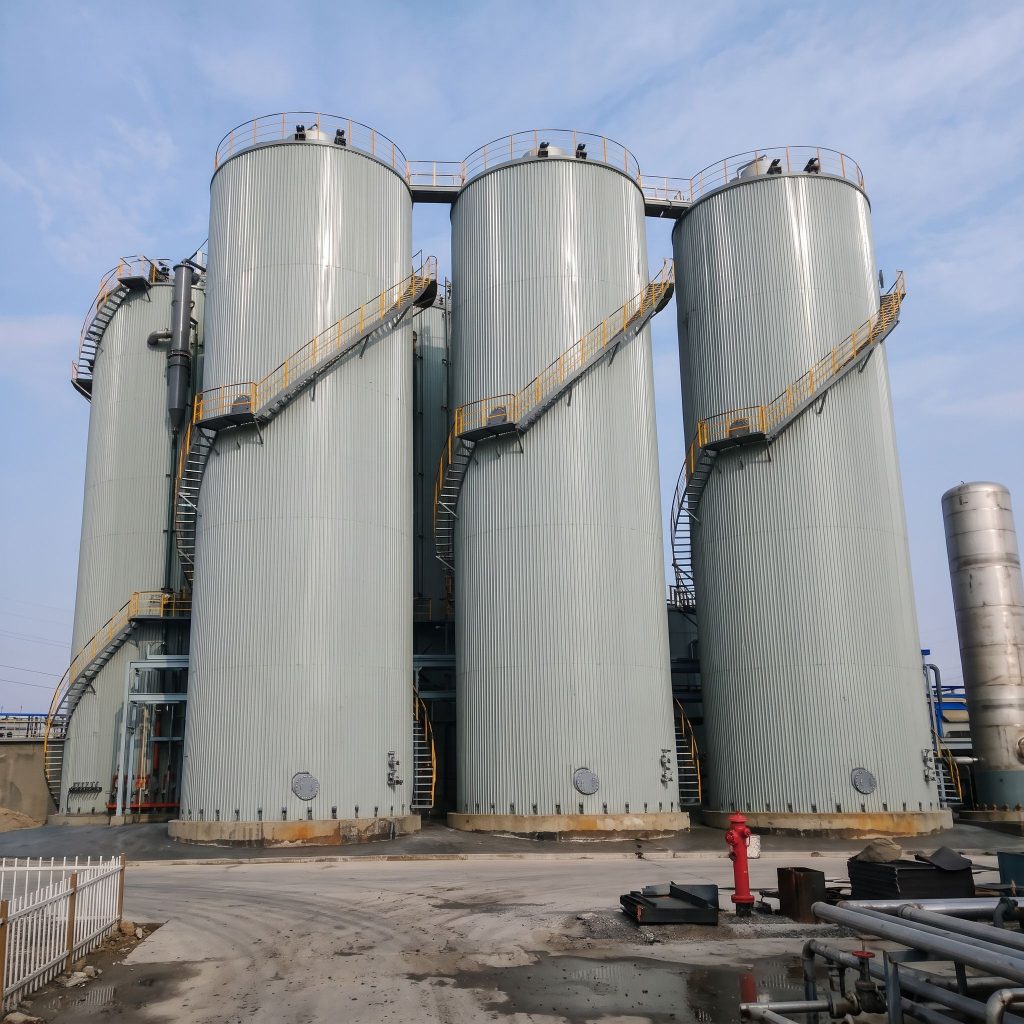
NPW HIGH-RATE IC & UASB ANAEROBIC REACTOR SERIES (BIOGAS ENERGY RECOVERY)
High-load anaerobic reactors digesting high-COD wastewater into clean methane biogas.
View product →
 WASTEWATER TREATMENT EQUIPMENT
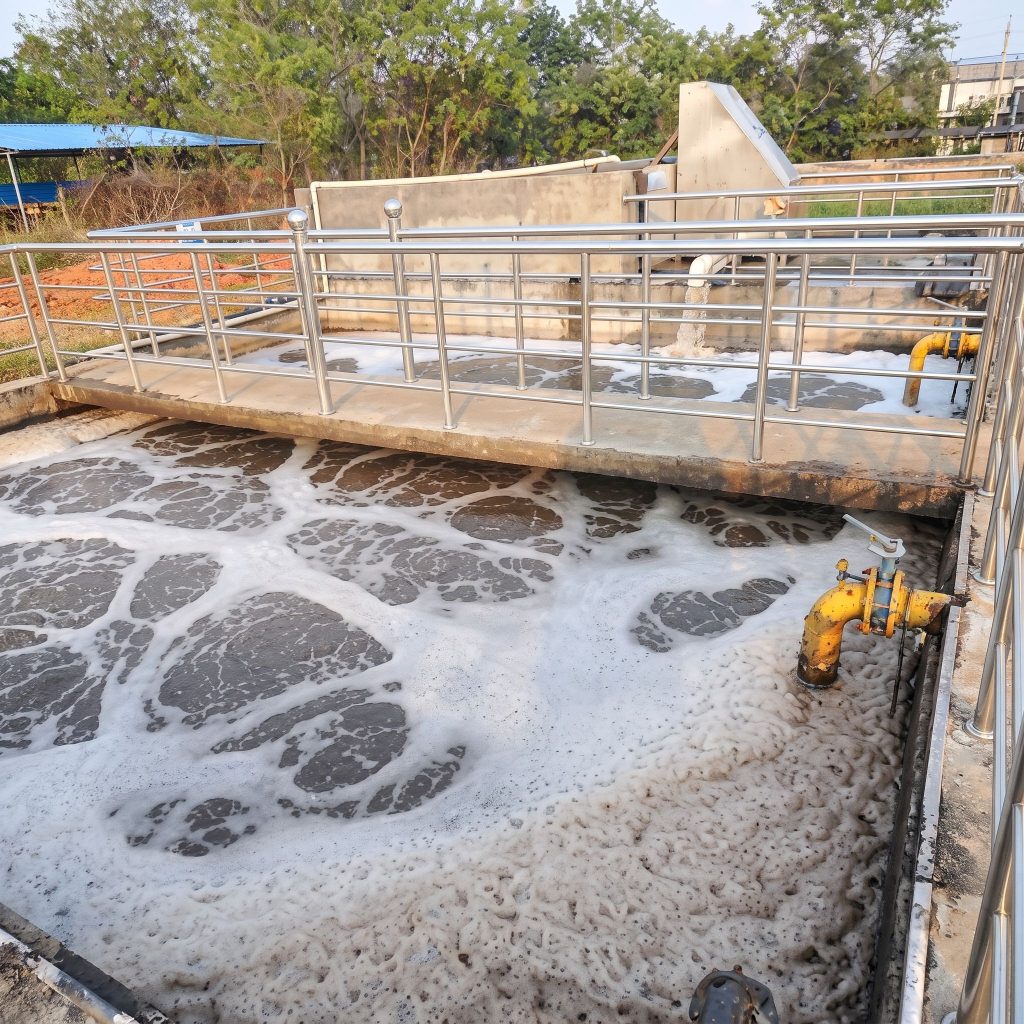
NPW HIGH-EFFICIENCY SHALLOW DISSOLVED AIR FLOTATION SYSTEM
Circular zero-speed shallow DAF clarifiers combining shallow tank theory with helical rotating scoops for high-volume wastewater clarification.
View product →
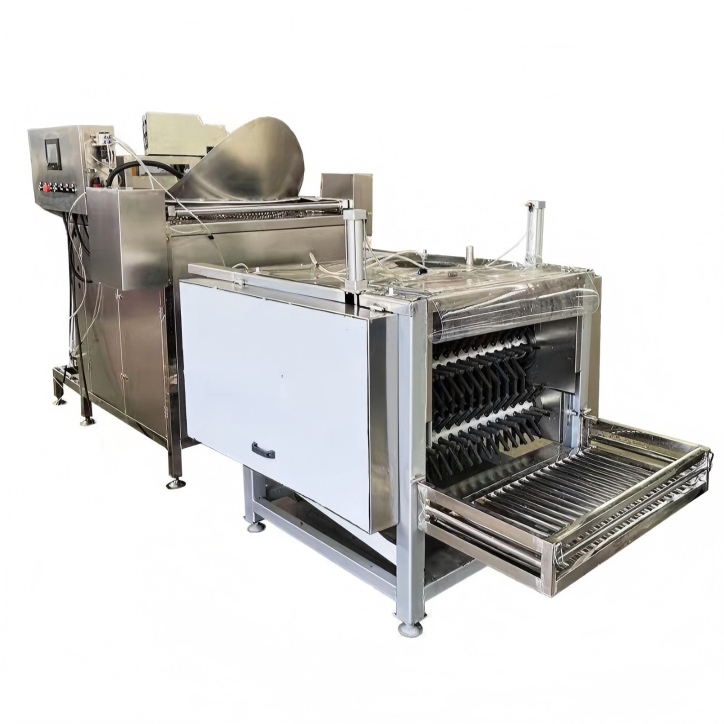 SCALDING AND PLUCKING MACHINE
NPW Automatic Poultry Processing Line: Bleeding, Scalding & Plucking System
Upgrade your slaughterhouse efficiency with NPW Equipment's fully automatic poultry processing line. This integrated system combines a…
View product →
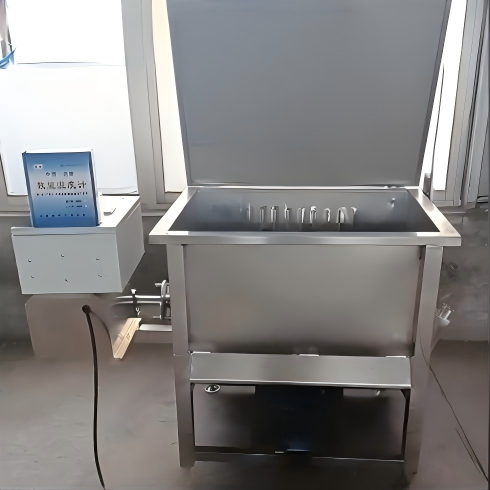 POULTRY SLAUGHTER EQUIPMENT
Automatic Temperature Control System
Our Automatic Temperature Control System delivers precise, real-time thermal regulation for industrial processes, ensuring optimal product quality…
View product →