Introduction to the 0.5T/H Reverse Osmosis System
In the food and beverage industry, water quality is paramount. The 0.5T/H reverse osmosis (RO) system from NPW is engineered to deliver high-purity water for a wide range of processing applications. With a capacity of 0.5 tons per hour, this compact yet powerful system is ideal for small to medium-scale operations, ensuring consistent water quality that meets stringent food safety standards.
Key Features and Benefits
- High-Efficiency Filtration: The system utilizes advanced RO membranes to remove up to 99% of dissolved salts, bacteria, and organic compounds, producing water that is safe and pure.
- Durable Construction: Built with food-grade stainless steel components, the system resists corrosion and ensures long-term reliability.
- Intelligent Control: Equipped with a PLC control panel, the system offers automated operation, real-time monitoring, and easy adjustment of parameters.
- Compact Design: The skid-mounted structure saves floor space and simplifies installation, making it suitable for facilities with limited areas.
- Low Maintenance: Designed for easy access to filters and membranes, reducing downtime and maintenance costs.
Applications in Food Processing
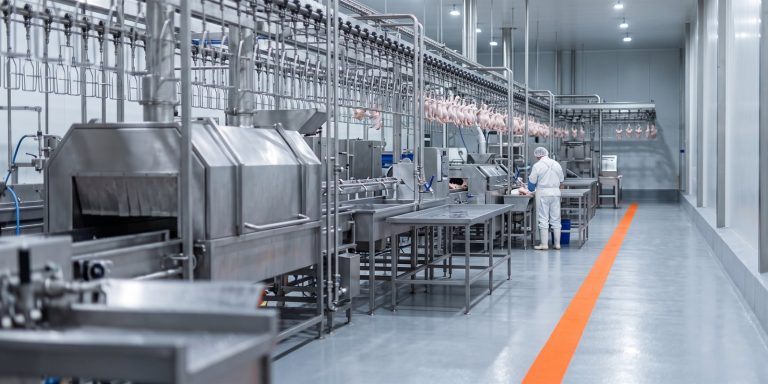
This RO system is widely used in food processing for:
- Ingredient Water: Providing pure water for mixing, blending, and product formulation.
- Beverage Production: Ensuring consistent taste and quality in juices, soft drinks, and bottled water.
- Equipment Cleaning: Supplying high-purity water for CIP system cleaning to prevent contamination, and pairing with a foam sanitation satellite for thorough surface hygiene.
- Boiler Feed: Reducing scale buildup and improving energy efficiency in steam generation, making it a dependable choice for boiler feed water treatment.
“Water is the most critical ingredient in food production. Our 0.5T/H RO system guarantees that every drop meets the highest purity standards, safeguarding both product quality and consumer health.” – NPW Engineering Team
Why Choose NPW’s Reverse Osmosis System?
NPW has been a trusted name in food processing equipment for decades. Our 0.5T/H RO system combines cutting-edge technology with robust construction to deliver unparalleled performance. Each unit undergoes rigorous testing to ensure it meets international quality benchmarks. With NPW, you invest in a solution that enhances operational efficiency, reduces costs, and ensures compliance with food safety regulations. It also integrates smoothly with your hygiene line, from wash-down stations for food processing boots to clean-in-place routines.
Conclusion
For food processors seeking a reliable, efficient, and compact water purification solution, the NPW 0.5T/H reverse osmosis system is the ideal choice. Contact us today to learn more about how this system can elevate your production standards.